

Testing standard
ISO 6502-3
Rubber — Measurement of vulcanization characteristics using curemeters — Part 3: Rotorless curemeter
Written and technically reviewed by Dak System Inc. engineeringLast reviewed
ISO 6502-3 is the rotorless cure meter test for rubber. Uncured compound is sealed between two heated dies, the lower die oscillates through a small fixed arc, and the torque transmitted through the rubber is recorded as it crosslinks. The rising trace is the cure curve, giving ML, MH, scorch time, t'c(90) and a cure rate index — the routine batch-acceptance test for a compound.
At a glance
- Test type
- Cure & rheology — how a rubber compound cures is tracked as it happens
- Published by
- ISO
- Edition
- ISO 6502-3:2023
- Material
- Rubber, elastomers & foams
- Runs on
- MDR
What the test does
Uncured compound is sealed inside a cavity between two heated dies rather than gripped. The lower die oscillates through a small fixed rotary arc while the torque transmitted through the rubber is recorded continuously. As crosslinks form the compound stiffens in shear and the torque rises, so the trace of torque against time is the cure curve for that compound at that temperature.
What it measures, and why it matters
The curve yields minimum torque (ML), maximum torque (MH), scorch time (ts), the time to ninety percent of torque rise (t'c(90)) and a cure rate index. ML flags a mis-mixed or ageing batch before it reaches the press. Scorch time sets the safe mould-filling window; t'c(90) sets the press cycle, since demoulding early leaves an undercured part. MH tracks crosslink density and therefore service stiffness. Together they are the routine batch-acceptance test for a rubber compound.
The specimen
- Preparation
- Cut from a milled sheet to slightly overfill the cavityThe closing dies form the geometry, so no precision cutting is involved.
- Die faces
- Biconical, cut with radial groovesWithout the grooves and the closing force the compound slips at the die face and the recorded torque understates the compound.
- Cavity
- Sealed under positive pneumatic pressure
- Rest period after mixing
- Fixed by the laboratory and kept toDakThe compound is reactive. A varying wait between mixing and testing is measured as scorch variability.
Oscillation and temperature
There is no crosshead. What has to be held is the kinematics and, above all, the die temperature.
- Frequency
- 1.667 Hz — one hundred cycles per minuteThe conventional setting, and reported with the result.
- Arc
- ±0.5°, about ±7 % shear strainCompliant instruments offer ±0.5°, ±1° and ±2°; some a much wider ±0.01° to ±20°.
- Both are reported
- Frequency and amplitudeBoth move the torque values, so neither is left to the operator.
- Die temperature
- About 100 °C to 200 °C
- Temperature control
- About ±0.3 °C, with quick recoveryCure rate roughly doubles per 10 °C, so a degree of error moves every time on the curve.
- Force capacity
- Not applicableNothing is pulled. The measured quantity is torque — a soft compound sits at a fraction of a decinewton metre at ML, so resolution at the bottom matters more than headroom at the top.
Reading the cure curve
ΔM = MH − ML
- MH
- maximum torque, dN·m — tracks crosslink density and service stiffness
- ML
- minimum torque, dN·m — flags a mis-mixed or ageing batch before it reaches the press
CRI = 100 / (t'c(90) − ts)
- t'c(90)
- time to ninety percent of torque rise, minutes — sets the press cycle
- ts
- scorch time, minutes — sets the safe mould-filling window
A high index means a fast cure with a narrow processing window, and it predicts whether a compound will tolerate a press running a few degrees hot.
How the test runs
- 01Bring the dies to the set temperature and let them stabilise.
- 02Cut a blank from milled sheet, sized to slightly overfill the cavity.
- 03Observe the laboratory's fixed rest period since mixing.
- 04Load and close the dies, sealing and pressurising the cavity.
- 05Start oscillation at 1.667 Hz through the set arc.
- 06Record torque against time as the compound warms, softens to ML, then stiffens.
- 07Continue until the torque plateaus, reverts, or the set time expires.
- 08Read ML, MH, scorch time and t'c(90) from the trace.
- 09Compute the cure rate index.
- 10Run a duplicate where the result releases a batch.
See the instrument
The instrument this method needs
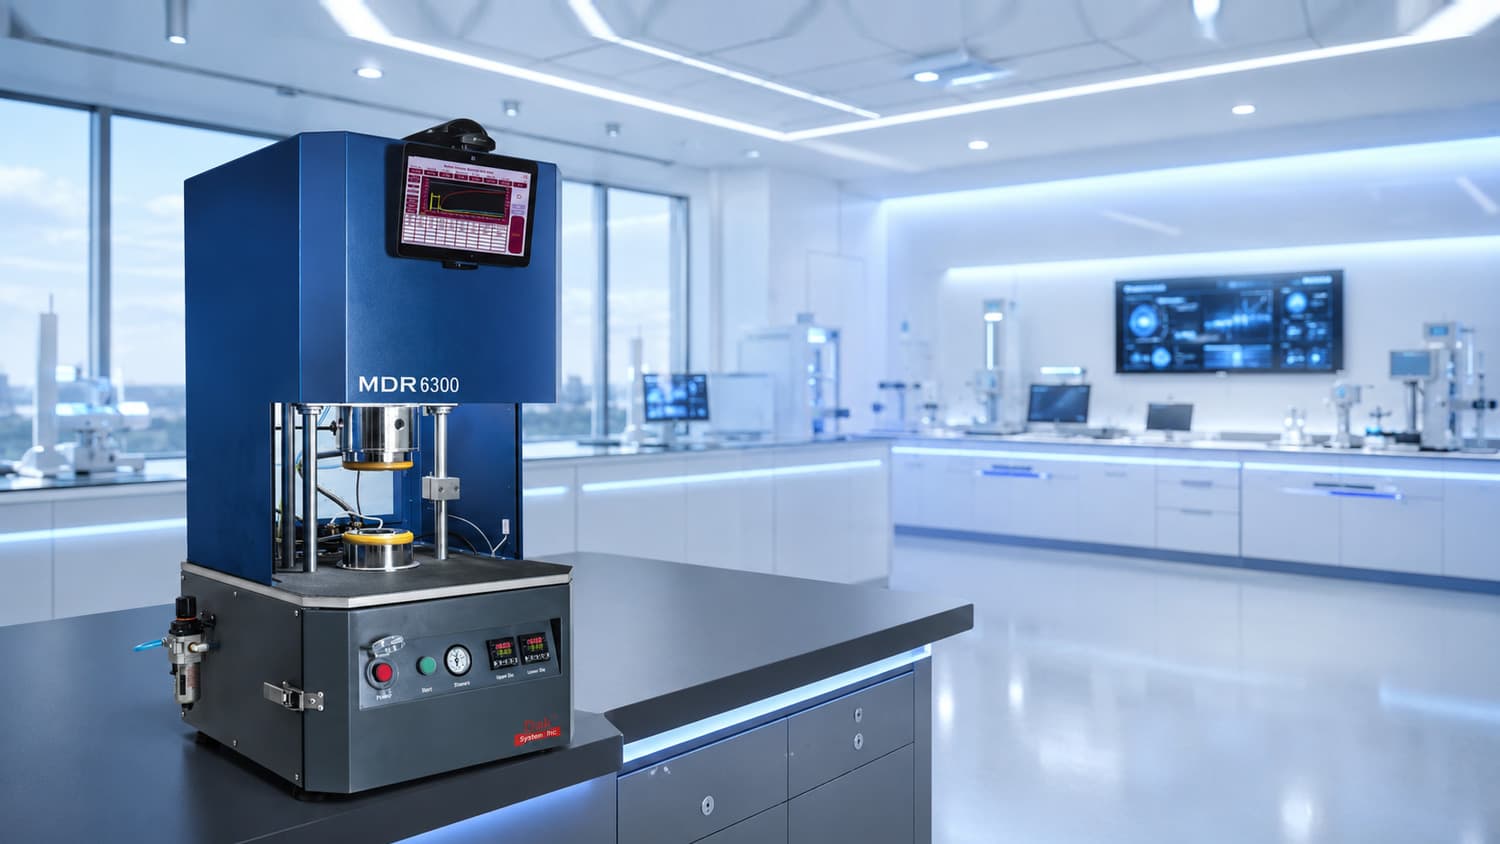
What the report has to contain
- Reference to ISO 6502-3
- Compound identification, batch and time since mixing
- Die temperature
- OSCILLATION FREQUENCY AND ARC — both move the values
- ML and MH
- Scorch time and t'c(90)
- Cure rate index
- Total test duration, and whether the curve plateaued or reverted
- Number of specimens
What the machine must be capable of
Nothing is pulled, so no force capacity and no force-accuracy class applies; the measured quantity is torque. A soft uncured compound sits at a fraction of a decinewton metre at ML and a stiff vulcanisate typically reaches 10 to 30 dNm at MH, against instrument spans quoted at roughly 0.001 to 250 dNm — so clean resolution at the bottom of the range matters more than headroom at the top. There is no crosshead motion and no extensometer: the test is isothermal and the kinematics are fixed. The conventional setting is oscillation at 1.667 Hz, one hundred cycles per minute, through ±0.5° of arc, approximately ±7 % shear strain; compliant instruments offer ±0.5°, ±1° and ±2°, some a much wider ±0.01° to ±20°. Both frequency and amplitude move the torque values, so both are held and reported rather than left to the operator. The fixture is the method: two biconical dies forming a sealed cavity closed under positive pneumatic pressure, their faces cut with radial grooves. Without the grooves and the closing force the compound slips at the die face and the recorded torque understates the compound. Die temperature is the other half — set points from about 100 °C to 200 °C, held to roughly ±0.3 °C with quick recovery after loading. No humidity control applies; the cavity is sealed.
What goes wrong in practice
Die slippage is the quiet one: worn or fouled grooves let the blank rotate against the die face and torque reads low across the whole curve. An underfilled cavity reaches the same place by a different route, giving low and unstable ML and MH. Scorch in storage advances the compound before it reaches the instrument, shortening ts and flattening the early curve. Die contamination from cured residue or torn interleaving film builds up over weeks and drifts MH downwards, which reads as a formulation change and is not.
ISO 6502-3 and ASTM D5289
| ISO 6502-3 | ASTM D5289 | ISO 6502-2 | |
|---|---|---|---|
| Instrument | Rotorless, sealed biconical dies | Rotorless, sealed or unsealed | Oscillating disc, with rotor |
| Frequency | 1.667 Hz conventional | About 1.667 Hz preferred | Lower |
| Arc | ±0.5° conventional | ±0.5° typical | Larger |
| Status | Routine batch acceptance | Routine batch acceptance | Largely displaced |
ISO 6502-3 and ASTM D5289 describe the same instrument class and are routinely cited alongside one another. The rotor-type curemeter is a different class and its numbers do not transfer — a specification written against historical oscillating-disc data cannot simply be applied to a rotorless curve.
Questions we are asked about this test
What is ISO 6502-3?
It is the international standard for measuring vulcanisation characteristics of rubber with a rotorless cure meter. Uncured compound is sealed between two heated dies, one of which oscillates through a small arc, and the torque transmitted through the rubber is recorded as it cures. The resulting cure curve is the routine batch-acceptance test for a compound.
What is the difference between ISO 6502-3 and ASTM D5289?
Very little in substance — they describe the same rotorless instrument class and are routinely cited alongside each other. Both use a sealed die cavity, a small oscillating arc and the same set of outputs. A laboratory equipped for one is equipped for the other, and specifications frequently name both.
Why are the die faces grooved?
To stop the compound slipping. A smooth die face lets uncured rubber shear against the metal rather than within itself, so the recorded torque understates the compound — and the error grows as the material stiffens. The radial grooves and the pneumatic closing force together ensure the deformation happens in the rubber.
Why does the oscillation arc have to be reported?
Because the torque values depend on it. A curve run at ±1° is not comparable with one run at ±0.5°, since a larger arc imposes more shear strain and reads higher torque. Compliant instruments offer several arcs, so the setting is part of the result rather than an instrument detail.
What does the cure rate index tell me?
How forgiving the compound will be in production. It is computed from the gap between scorch time and t'c(90), so a high index means the cure completes quickly once it starts — good for cycle time, but leaving a narrow window if the press runs a few degrees hot. A low index is slower and more tolerant.
Does this need a universal testing machine?
No. It needs a torsion-shear rheometer with heated biconical dies, pneumatic closure and fine torque resolution. Nothing is pulled and there is no force capacity to specify — the measured quantity is torque, and a soft compound sits at a fraction of a decinewton metre at ML, so resolution at the bottom of the range matters far more than headroom at the top.
Running ISO 6502-3 on the MDR
Both instruments run a sealed, pressurised cavity that prevents compound extrusion and holds the test volume exactly, so the torque trace reflects the material.
| The method asks for | Dak supplies | |
|---|---|---|
| Torque & frequency | Nothing is pulled — the instrument reads torque, not force: a soft uncured compound sits at a fraction of a dNm at the minimum (ML) and a stiff vulcanizate typically reaches somewhere between 10 and 30 dNm at maximum torque (MH), inside an instrument span that commercial MDRs quote as roughly 0.001 to 250 dNm. | Torque up to 20 N·m; the RPA Ultimo measures from 0.0001 N·m. MDR: ±0.5° arc as standard, at a fixed 1.667 Hz. RPA Ultimo: 0.0016–50 Hz, 0.05–90° arc. |
| Test cavity | Sealed biconical die cavity with an oscillating lower die (rotorless curemeter / MDR) | MDR: sealed biconical rotorless dies, closed pneumatically. RPA: a sealed, pressurised cavity |
| Temperature | Isothermal heated dies, working range about 100 °C to 200 °C, die temperature held to roughly ±0.3 °C | Room temperature to 230 °C; on the MDR, upper and lower dies are controlled separately |
This page describes the method as practised. The governing text is the current edition from the issuing body. Tell us what you are testing and we will answer with the machine, the fixture and a quotation.