
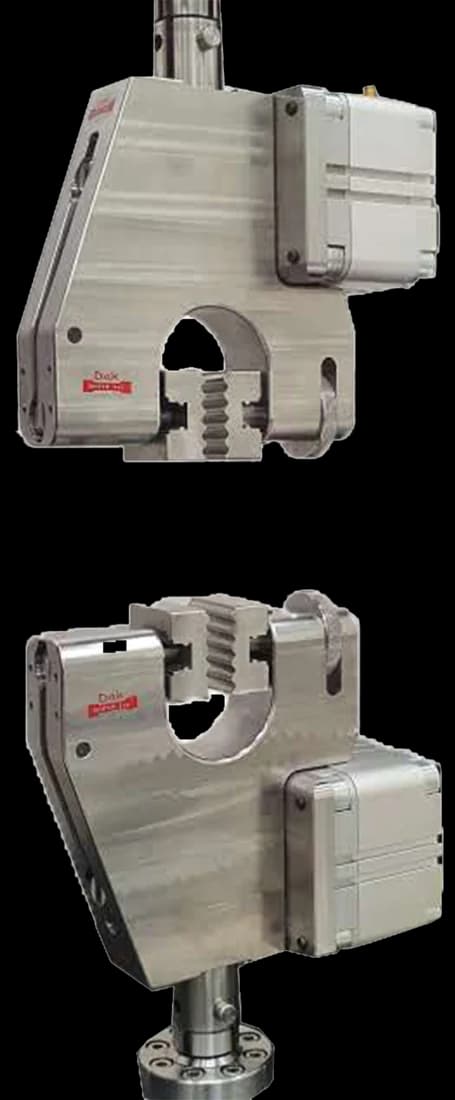
Standard 25 mm
Pneumatic Vice Action Grip
Constant air pressure across the full jaw face — the arrangement that holds a film without cutting it at the clamp line, and identical on every specimen.
Specifications
Testing standard
Standard Test Method for Tensile Properties of Thin Plastic Sheeting
Written and technically reviewed by Dak System Inc. engineeringLast reviewed
ASTM D882 is the tensile test for plastic film and thin sheeting up to 1.0 mm thick. A plain parallel-sided strip — no dumbbell waist — is pulled apart at a speed set by its expected elongation. It reports tensile strength, elongation at break, modulus, tensile energy to break and breaking factor, the force-per-width figure used where thickness cannot be gauged reliably.
A rectangular strip cut from film or thin sheet is clamped at both ends at a set grip separation. The crosshead moves at a constant rate and pulls the strip along its length until it breaks, while force and crosshead travel are recorded continuously. There is no narrow waist and no dumbbell — the specimen is a plain parallel-sided strip, so it may break anywhere along the free length.
The method reports tensile strength, elongation at break, modulus of elasticity, tensile energy to break and breaking factor. Strength and elongation are the routine lot-release pair for packaging film — a drop in elongation flags degraded resin or a drift in orientation. Modulus feeds stiffness and web-handling calculations. Breaking factor, force divided by width, is used where thickness cannot be gauged reliably. Tensile energy to break, the area under the curve, ranks toughness between grades that share a similar peak load.
There is no waisted section here, so the specimen can break anywhere along its free length — and the geometry rules exist to make sure it breaks for the right reason.
The speed is chosen from the expected elongation, and it moves with the grip separation — so speed and separation are picked together rather than independently.
TS = F_max / (w × t)
BF = F_max / w
Force per unit width, reported INSTEAD of tensile strength where thickness cannot be gauged reliably — thin gauge-variable film, coated webs, laminates. It avoids dividing by a number nobody trusts.
E = (extension / initial grip separation) × 100
Grip separation IS the reference length in this method, which is why the separation is a specified value rather than whatever the operator set.
TEB = area under the force–extension curve / specimen volume
Ranks toughness between grades whose peak loads are similar — the number that separates a film that tears from one that stretches.
Grip design matters more here than almost anywhere. Jaw faces that bite will cut a film at the clamp line, and faces that do not bite let it pull out — and both failures produce a curve that looks like a real test.
Constant air pressure across the full jaw face — the arrangement that holds a film without cutting it at the clamp line, and identical on every specimen.
Specifications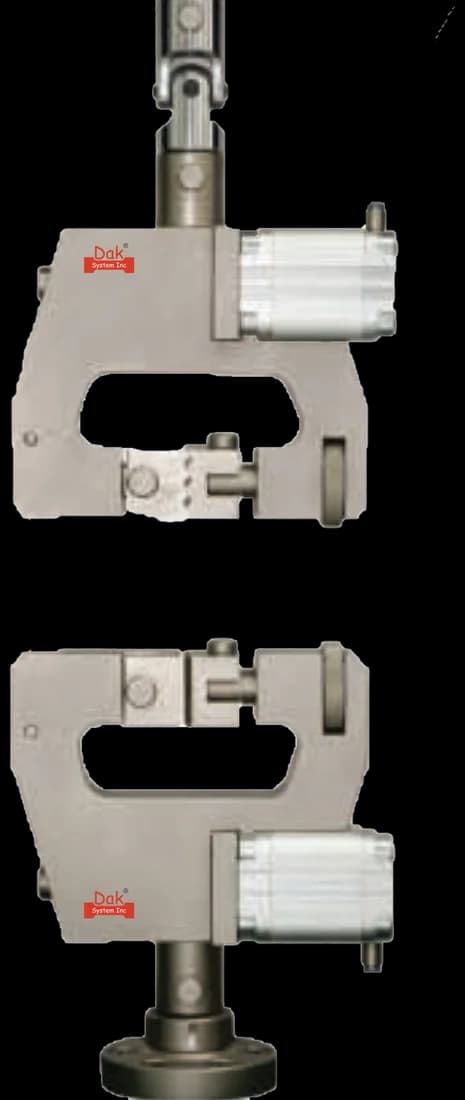
Light duty closure for the lowest forces, where a heavier grip would crush a delicate web before the test began.
SpecificationsLoads are low. A 25 mm strip of packaging polyethylene breaks well under 100 N, so a 500 N to 1 kN cell on a bench frame covers most of this work and resolution at the bottom of the scale matters more than capacity. The widest, thickest specimen the method admits — 25.4 mm at the full 1.0 mm in a strong oriented polyester — would demand several kN, so capacity is chosen against the material rather than against the method. Force indication must be verified to ASTM E4.
Speed is set by expected elongation, not by preference: an initial strain rate of 0.1 min⁻¹ at 125 mm separation (12.5 mm/min) below 20 % elongation, 0.5 min⁻¹ at 100 mm (50 mm/min) from 20 to 100 %, and 10.0 min⁻¹ at 50 mm (500 mm/min) above 100 %. The rate must hold within 5 % of the set value, so the frame needs genuine speed control at 500 mm/min under load. Modulus is run separately at 250 mm separation.
No extensometer is required — strain comes from grip separation. Polyolefin film routinely runs past 500 % though, so a high-elongation or non-contact device gives a cleaner total elongation than crosshead travel does.
Grips must minimise slippage and spread clamping stress evenly. Pneumatic vice-action or wedge grips with flat rubber faces suit fragile specimens, line-contact faces suit slippery ones, and roller grips — the strip wrapped round a rubber-faced drum against a compression bar — suit thin film specifically. Faces must be wider than the strip. Serrated steel faces are wrong here: they nick the film and start the failure at the jaw line.
Jaw-line tears are the dominant invalid result — the film fails where the faces bite instead of in the free length, so the number is a grip artefact. Slippage is the other half of the same problem: the strip creeps out under load, extension reads long and modulus reads low. An edge nick from a blunt cutter initiates the break early and depresses strength by a wide margin. Thickness variance across a web is the quiet one — stress is calculated from a measured thickness, so a gauge taken at one point misprices the whole specimen.
| ASTM D882 | ASTM D638 | ISO 527-3 | |
|---|---|---|---|
| Applies to | Film and sheet up to 1.0 mm | Above 1.0 mm | Films and sheets |
| Specimen | Plain parallel strip | Waisted dumbbell | Plain strip |
| Reference length | Grip separation | Marked gauge length | 50 mm gauge |
| Speed basis | Set by expected elongation | Tabulated by specimen type | Nominal speed series |
| Distinctive output | Breaking factor, N/mm width | Tensile modulus | Tensile modulus |
The 1.0 mm boundary is not advisory. Gripping thin film in a D638 dumbbell geometry produces tab failures rather than data, and the waist that helps a rigid plastic simply becomes another place for a thin web to fail.
It is the ASTM tensile test for thin plastic sheeting and film, up to 1.0 mm thick. A plain parallel-sided strip is pulled apart until it breaks, and the method reports tensile strength, elongation at break, modulus, tensile energy to break and breaking factor.
At 1.0 mm thickness. Below it, D882 applies; above it, D638. The boundary is not a formality — a thin film clamped in a D638 dumbbell geometry tends to fail at the tab rather than in the waist, so the test measures the grip. D882 uses a plain strip and a specified grip separation instead.
It is the maximum force divided by the specimen width, in newtons per millimetre, and it is reported instead of tensile strength wherever thickness cannot be gauged reliably — thin gauge-variable film, coated webs, laminates. It avoids dividing a good force measurement by a thickness nobody trusts, which is how an apparently precise strength figure ends up carrying someone else's measurement error.
It depends on the film's expected elongation, and it moves with the grip separation. Below 20 % elongation the test runs at 12.5 mm/min with 125 mm separation; from 20 to 100 % at 50 mm/min with 100 mm; above 100 % at 500 mm/min with 50 mm. The rate must hold within 5 % of the set value, so a frame needs real speed control at 500 mm/min under load.
Because in this method the grip separation IS the reference length that elongation is calculated from. There is no marked gauge on a plain strip and often no extensometer, so the distance between the jaws at the start is what the strain is referred to. Setting it arbitrarily makes the elongation figure meaningless.
A small one. A 25 mm strip of packaging polyethylene breaks well under 100 N, so a 500 N to 1 kN cell on a bench frame covers most of this work, and resolution at the bottom of the scale matters far more than capacity. The heaviest case the method admits — 25.4 mm at the full 1.0 mm in a strong oriented polyester — would demand several kN, so capacity follows the material rather than the method.
Jaw faces that bite too hard cut the film at the clamp line; faces that do not bite let it pull out. Both are common with film and both produce a curve that looks like a genuine test, which is why the specimen has to be inspected after every break. A break at the jaw line is invalid under the method and must be replaced rather than averaged in.
For any oriented film, yes. Blown and cast films are anisotropic, so machine-direction and transverse-direction results differ, sometimes by a large factor. The direction tested has to be reported, and a single figure quoted without it does not describe the film.
Dak verifies against whichever standard the method names, and where a class applies our frames sit a class tighter than it asks.
| The method asks for | Dak supplies | |
|---|---|---|
| Capacity | Thin sheeting parts at low load — a 25 mm wide strip of packaging polyethylene breaks well under 100 N — so the useful range is a load cell of 500 N to 1 kN on a single- or twin-column bench frame, and force resolution at the bottom of the scale matters far more than capacity. The widest, thickest specimen the method admits, 25.4 mm at the full 1.0 mm thickness in a strong oriented polyester, would demand several kN, so capacity is chosen against the material rather than the method. | Load cells from 1 kg to 60 ton on the Series 7200, and 0.5 to 100 kN on the Series 9000 |
| Force accuracy | ASTM E4 | Verified to ASTM E4, and to ISO 7500-1 Class 0.5 |
| Gripping | Pneumatic vice or wedge grips with flat rubber or line-contact faces, or roller grips, at a set grip separation | Our vice-action grips or self-tightening eccentric roller grips, built to the specimen |
| Environment | Condition at least 40 h at 23 °C / 50 % RH per ASTM D618 Procedure A and test in the same atmosphere | 3009 series chambers, −150 °C to +400 °C — temperature only |
This page describes the method as practised. The governing text is the current edition from the issuing body. Tell us what you are testing and we will answer with the machine, the fixture and a quotation.